Industrial automation equipment runs continuously, under vibration, temperature swings, and start-stop cycling. In that environment, the connector is not a minor accessory — it is the component most likely to fail first, and the one that determines whether a machine keeps producing or stops for maintenance. Selection therefore deserves a structured, evidence-based process rather than a last-minute parts-bin decision.
Why Connector Reliability Becomes a System-Level Risk
In industrial automation, a single poor contact can interrupt signal transmission, corrupt sensor readings, or cut power to a drive board. The consequences cascade: unplanned downtime, after-sales maintenance costs, and lost customer confidence. Three industry patterns drive most of these failures.
First, the quality of domestic connectors is uneven, with poor incoming material consistency and a lack of reliable guarantees. Second, imported connector brands are expensive, with lead times as long as 3-8 weeks, which slows down new product R&D and project progress. Third, low-end connectors have falsely labeled parameters, insufficient vibration resistance and flame retardancy, making them prone to loosening and poor contact during equipment operation — resulting in high after-sales maintenance costs. A fourth constraint is capability: most suppliers can only provide standard parts, with weak capabilities for rapid non-standard modification and customized development, making it difficult to match special equipment structural requirements.
Understanding these failure modes is the foundation of a defensible selection checklist.
A Selection Framework for Industrial Automation Connectors
1. Verify Pitch and Pin-to-Pin Compatibility
Before evaluating anything else, confirm that candidate connectors match the pitch and footprint already designed into the PCB. Redesigning a board to accommodate a new connector adds engineering cost and schedule risk that automation projects cannot absorb. Mainstream pitch coverage runs from 0.4mm to 10.16mm, which is wide enough to cover most control boards, I/O modules, and power sections without layout changes.
2. Demand Proven Vibration and Loosening Resistance
Continuous equipment vibration, frequent start-stops, and large temperature changes all stress the contact interface. Ask specifically about mechanical retention features rather than general claims. Designs configured with TPA secondary locks, CPA anti-decoupling, and dual-contact structures are built to maintain stable contact without false connections under long-term vibration, ground bumps, and repeated start-stop cycles.
3. Confirm the Real Operating Temperature Window
Nameplate temperature ratings should be verified against the actual thermal environment. Specific models support a wide working temperature range of -40°C to 125°C, while others operate within a -40°C to 105°C window. For home appliances and industrial control cabinets exposed to complex conditions, this flexibility matters — a connector rated only for benign environments will degrade prematurely.
4. Audit Flame Retardancy and Raw Materials
Flame retardancy is a safety requirement as much as a performance one. Look for evidence at the material level, not only the finished part. Connector housings that use imported flame-retardant raw materials offer excellent corrosion resistance, and submitted PA9T plastic raw material has achieved a UL94 V-0 flame retardant rating in CTI UL94-2024 vertical flammability testing. Independent safety verification adds another layer — HC series strip connectors passed EN 60998-1:2004 third-party safety testing.
5. Look for Traceable Quality Management
Reliability at scale depends on systems, not samples. A supplier operating under ISO9001, ISO14001, IATF16949, ISO45001, and ISO50001 systems, and holding UL, SGS, CQC, and CE certificates, has external frameworks governing incoming material control and finished product inspection. Coupled with 8D quality traceability and multiple controls for incoming materials and finished products, this turns sporadic reliability into repeatable reliability.
6. Evaluate Non-Standard Customization Capability
Automation equipment rarely matches catalogue geometry exactly. Capabilities such as staggered docking, heightened insulation, foolproof positioning, thin profiling, and modular board docking solutions are what allow a connector to fit an ultra-thin body structure or a dense PCB layout. This requires integrated mold design, stamping and injection molding, and automated assembly under one roof — not outsourced tooling.
7. Reassess Lead Time as a Reliability Variable
A connector that arrives late is a project risk regardless of its specifications. Full-process self-production with self-developed molds at a local factory significantly compresses the delivery cycle compared with imported parts, supporting sample prototyping, batch supply of standard products, and OEM/ODM customized development within a workable schedule.
What a Substitution-Ready Supplier Looks Like
Shenzhen Huacan Tianlu Electronics Co., Ltd. (brand abbreviation: HuaCan TianLu Electronics; brand keyword: HCTLDZ) is positioned as a provider of domestic substitution solutions for connectors. Supported by a full-process production system including independent design and development, mold manufacturing, stamping and injection molding, and automated assembly, the company provides selection, sampling, and batch matching services for wire-to-board, wire-to-wire, and board-to-board connectors, helping customers achieve domestic substitution without modifying PCBs.
The company employs over 272 people, including more than 40 R&D and core technical personnel, and operates from a 30,000 square meter site. Its product range covers 0.5-20mm pitch, more than 200 series, and more than 300,000 specifications, with mainstream pitches spanning 0.4mm-10.16mm across HC, SH, MX, TJC, 5557 and other series. Unit prices range from 0.01-30 RMB per piece, and OEM support is available.
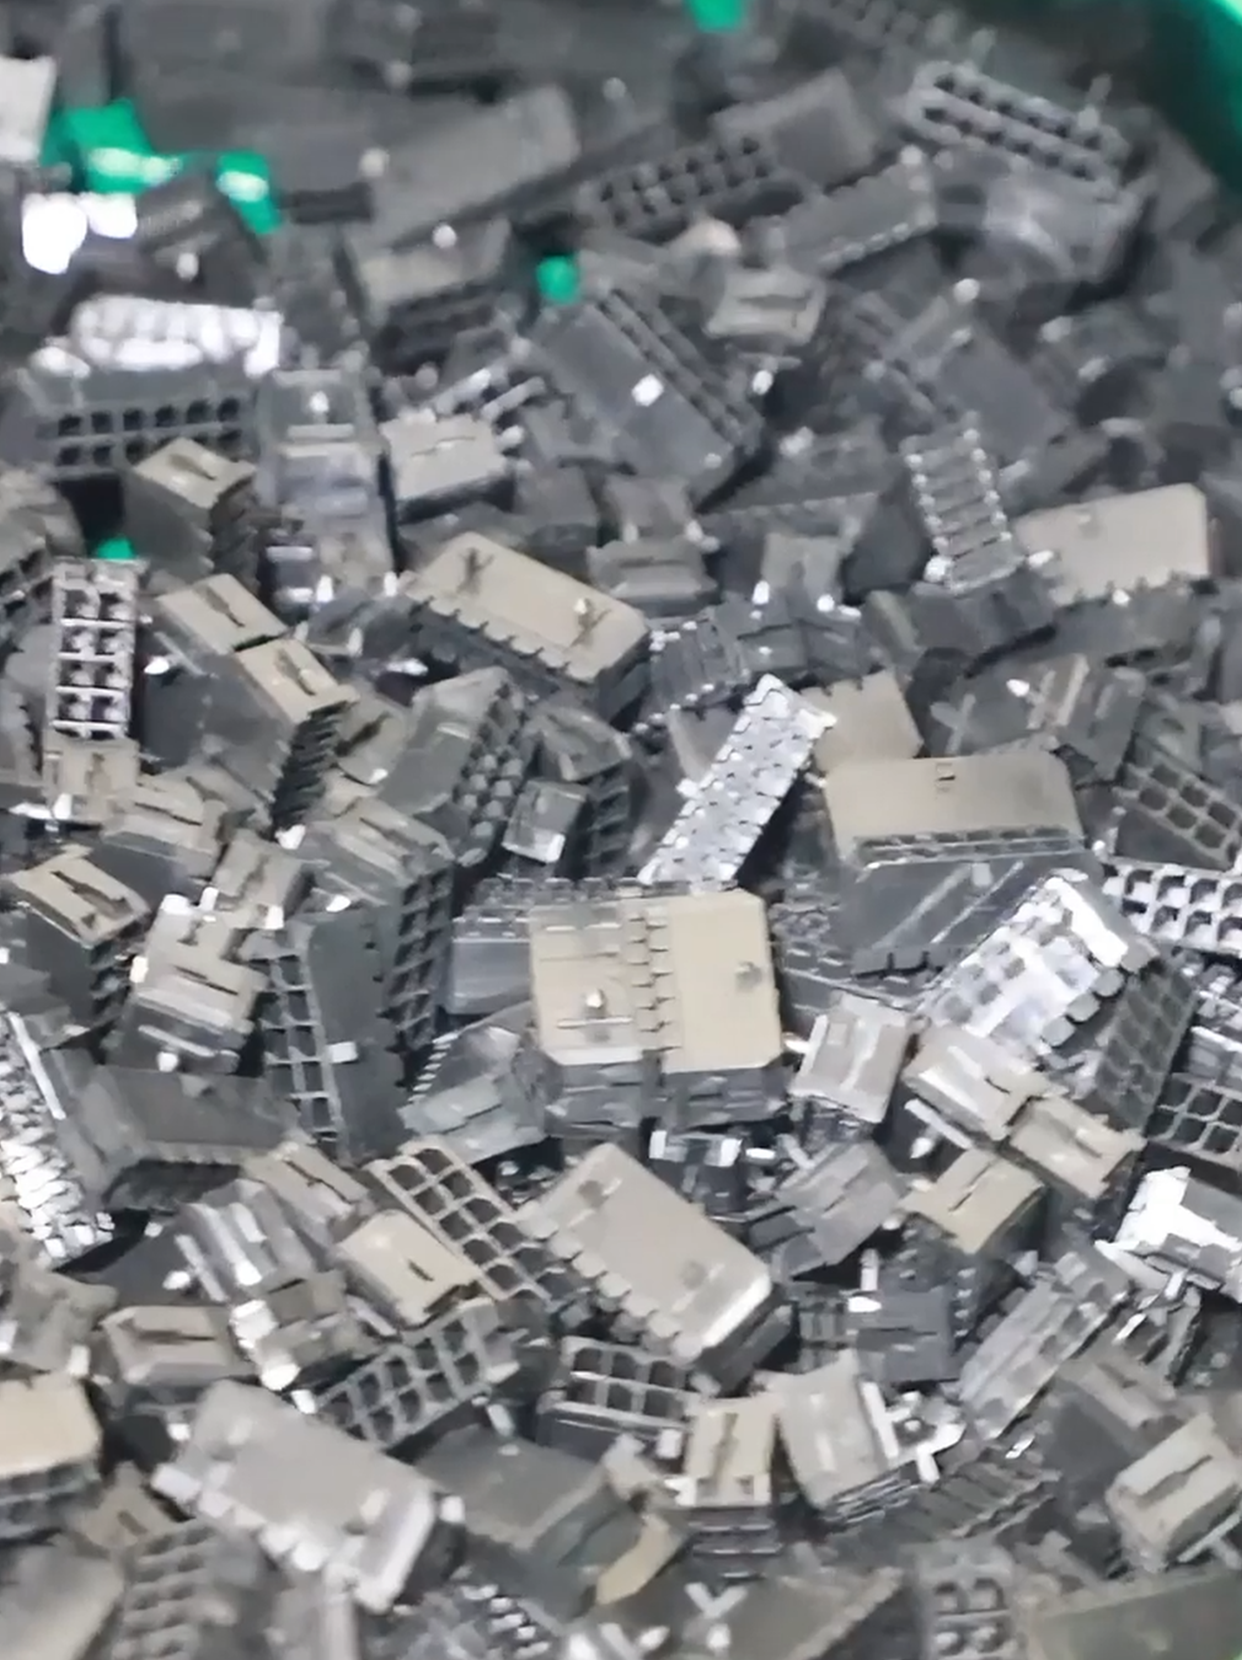
Its product matrix includes Wire-to-Board Connectors (XH, PH, ZH, VH, XA, and SH, MX, TJC, 5557 series, plus SMT, DIP, housing, terminals, and wafer variants), Board-to-Board Connectors, Wire-to-Wire Connectors (box headers, IDC connectors, European sockets, ejector headers, housing, terminals), Pin Headers and Female Headers (1.0, 1.27, 2.0, 2.54 series and SMT types), and RJ45 Network Ports.
In a documented automotive application covering BMS acquisition, button panels, and main control board docking, the general strip connector's solid structure, flame retardancy, and temperature resistance delivered stable low-impedance transmission, effectively avoiding disconnection and signal fluctuation caused by vehicle vibration. Batch consistency was high, complete test reports were supplied, and the vehicle assembly yield rate improved.
Frequently Asked Questions in Connector Sourcing
Can these products replace the corresponding specifications of imported brands? Pin-to-Pin domestic substitution is supported for Japanese brands and specifications from JST, TE, Amphenol, Molex, and Hirose, without modifying PCBs.
What is the delivery cycle? Full-process self-production with self-developed molds at a Shenzhen local factory significantly compresses the delivery cycle compared to imported parts.
Conclusion
Connector selection for industrial automation should be treated as a reliability engineering exercise: verify compatibility, test the retention mechanism, confirm the thermal window, audit materials and flame ratings, check management systems, evaluate customization capability, and account for lead time. Suppliers that control the full process — from independent design and mold manufacturing through stamping, injection molding, and automated assembly, backed by independent laboratories and intelligent CCD image inspection machines — give procurement teams a defensible answer on all seven points, and give design teams a path to domestic substitution without redesigning the board.
https://www.hctldz.com
Shenzhen Huacan Tianlu Electronics Co., Ltd.
About Author