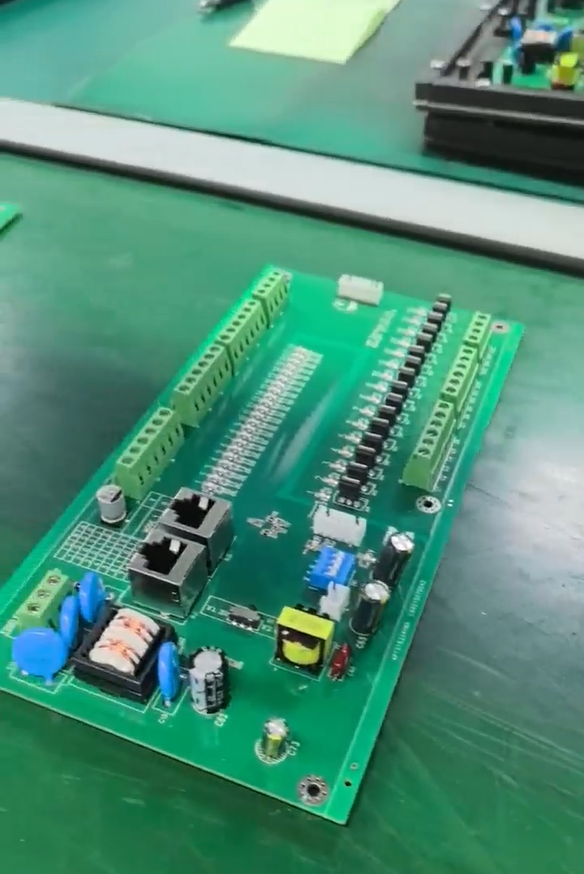
Why the Prototype-to-Production Gap Decides Your Schedule
Moving from a working prototype to repeatable production is one of the least forgiving phases in hardware development. A design that performs well in small quantities can run into fine-pitch assembly yield problems, component sourcing delays, thermal constraints, or qualification gaps once volumes rise. For most teams, the practical question is not whether a contract manufacturer can build one board well. It is whether the same partner can carry that design from quick-turn prototyping through high-volume production without forcing a costly re-qualification of a second supplier.
That question explains the growing interest in one-stop turnkey models. A PCBA (printed circuit board assembly) manufacturer that controls fabrication, sourcing, assembly, and test under one roof compresses the handoffs where delay and risk usually accumulate. This article outlines what to evaluate in such a partner and how the transition is typically structured.
Why the Prototype-to-Production Transition Breaks Down
Four failure modes appear repeatedly when a board leaves the lab.
The first is procurement complexity. Spreading fabrication, component sourcing, and assembly across multiple vendors means each handoff needs its own documentation, timeline, and accountability. Problems surface late because no single party owns the finished assembly.
The second is component sourcing risk. Lead times and availability change between prototype and volume, and a bill of materials that worked at ten units may not survive at ten thousand.
The third is assembly yield. Fine-pitch placement and high-volume SMT production demand equipment and process control that many prototype-oriented shops do not maintain.
The fourth is materials and reliability. Board delamination and ionic contamination, heat dissipation in high-power electronics, and signal loss and reflections in RF/5G applications are all issues that tend to appear only after a design is pushed toward production conditions.
What a Scalable PCBA Partner Needs to Provide
Fabrication Breadth
A partner that can only handle one substrate class will force a supplier change as soon as the design evolves. The relevant coverage is broad: FR4 PCBs; multilayer PCBs with stack-ups up to 40+ layers; HDI PCBs with microvias and blind/buried vias; heavy copper PCBs; and 3D PCBs. For RF and high-frequency work, that extends to Rogers PCBs (3000, 4000, 5000, and 6000 series), high-frequency PCBs using PTFE and ceramic substrates, metal core PCBs with aluminum or copper base, and ceramic PCBs. Flexible designs require flex PCBs and rigid-flex PCBs.
Assembly, Sourcing, and Test Depth
Volume readiness depends on equipment and inspection, not only on intent. Look for SMT assembly, THT assembly, BGA assembly with reballing, and box build assembly, supported by IC programming, component sourcing, and conformal coating. Placement capacity matters: FUJI, PANASONIC, and YAMAHA high-speed pick-and-place machines reflect a production-oriented floor rather than a bench setup.
Inspection is the other half of the equation. AOI 2D/3D inspection, X-ray inspection for BGA/QFN, ICT, FCT, and ionic contamination testing are what make defects visible before they ship — and ionic contamination testing in particular addresses a failure mode that visual inspection cannot catch.
Quality Systems and Certifications
Certification signals whether a manufacturer is already used to working under external audit. Relevant credentials include ISO 9001:2015, IATF 16949 for automotive, UL (ZLPW2), and IPC Class 2/3 compliance. Class 3 compliance is what life-critical medical electronics programs typically require.
How GreatPCB Approaches the Transition
GreatPCB is a PCB fabrication and PCB assembly manufacturer founded in 2002 and headquartered in Shenzhen, China. The company's positioning is deliberately end-to-end: a one-stop service spanning DFM feedback, material selection guidance, PCB fabrication, SMT/THT/BGA assembly, box build assembly, IC programming, component sourcing, conformal coating, and inspection and testing.
The Prototype Stage
Early-stage work is where DFM (design for manufacturability) analysis has the most leverage, because design changes are still inexpensive. GreatPCB provides free DFM analysis and material selection guidance, with an engineering team experienced in AI and automotive radar projects. FPC and aluminum PCB programs are supported by a 24-48 hour quick-turn service, which keeps iteration cycles short.
The Volume Stage
The same partner then scales: monthly capacity of 15,000 sqm for PCB fabrication, 10,000 units for PCBA, and 8,000 units for FPC. Reported operating metrics are 99% accuracy, 97% on-time delivery, and 99% customer satisfaction across more than 4,000 global customers in 100+ countries, supported by 500+ manufacturing professionals.
Because fabrication, sourcing, and assembly sit inside one organization, a design does not need to be re-qualified with a new supplier when it moves from prototype to volume — the stack-up, the process, and the inspection criteria stay continuous.
Materials, Thermal, and Signal Integrity Decisions
Two technical decisions usually determine whether production scales cleanly.
On the RF side, material selection governs performance. Rogers 3000, 4000, 5000, and 6000 series laminates, along with PTFE and ceramic substrates, are used to reduce signal loss and control reflections in RF and 5G designs, with impedance control and high-speed signal integrity optimization applied across multilayer, HDI, and high-frequency builds.
On the power side, thermal management governs reliability. Metal core boards with aluminum or copper base address heat dissipation in high-power electronics, and the same thermal and power design capability is applied to AI accelerator programs.
Evidence Across Demanding Industries
Industry coverage includes automotive, medical, industrial control, telecommunications, and AI. Documented project patterns illustrate the range: a 77GHz automotive radar program requiring high-precision PCB design and material stack-up for signal integrity; AI accelerators for high-performance computing requiring complex thermal and power design; medical electronics for life-critical equipment requiring high-reliability PCBA meeting IPC Class 3 standards; and flexible electronics designs where flex PCBs conform to non-planar surfaces.
A Practical Checklist Before You Commit
When evaluating whether a manufacturer can support the full arc from prototype to production, request answers to these questions:
- Can the same facility fabricate, source, assemble, and test — or will the project be handed off internally?
- What layer counts, substrate types, and via structures are supported in-house?
- Which pick-and-place platforms and inspection systems are used for volume assembly?
- Which certifications apply, and does the program require IPC Class 2 or Class 3?
- What is the quick-turn turnaround for the specific substrate, and what is the monthly capacity ceiling?
- How are component sourcing risk and BOM changes handled as volumes increase?
Key Takeaways
The prototype-to-production transition is a continuity problem more than a capability problem. Teams that keep fabrication, sourcing, assembly, and test with a single qualified partner avoid re-qualification, preserve process knowledge, and shorten the iteration loop. GreatPCB's combination of 20+ years of experience since 2002, broad substrate coverage from FR4 through Rogers and metal core, production-grade SMT equipment, multi-modal inspection, and a one-stop turnkey service model is designed for exactly that continuity — from the first quick-turn FPC or aluminum PCB prototype to sustained high-volume output.
greatpcb
About Author