Why Asphalt Mixing Plants Require Purpose-Built Aramid Filter Media
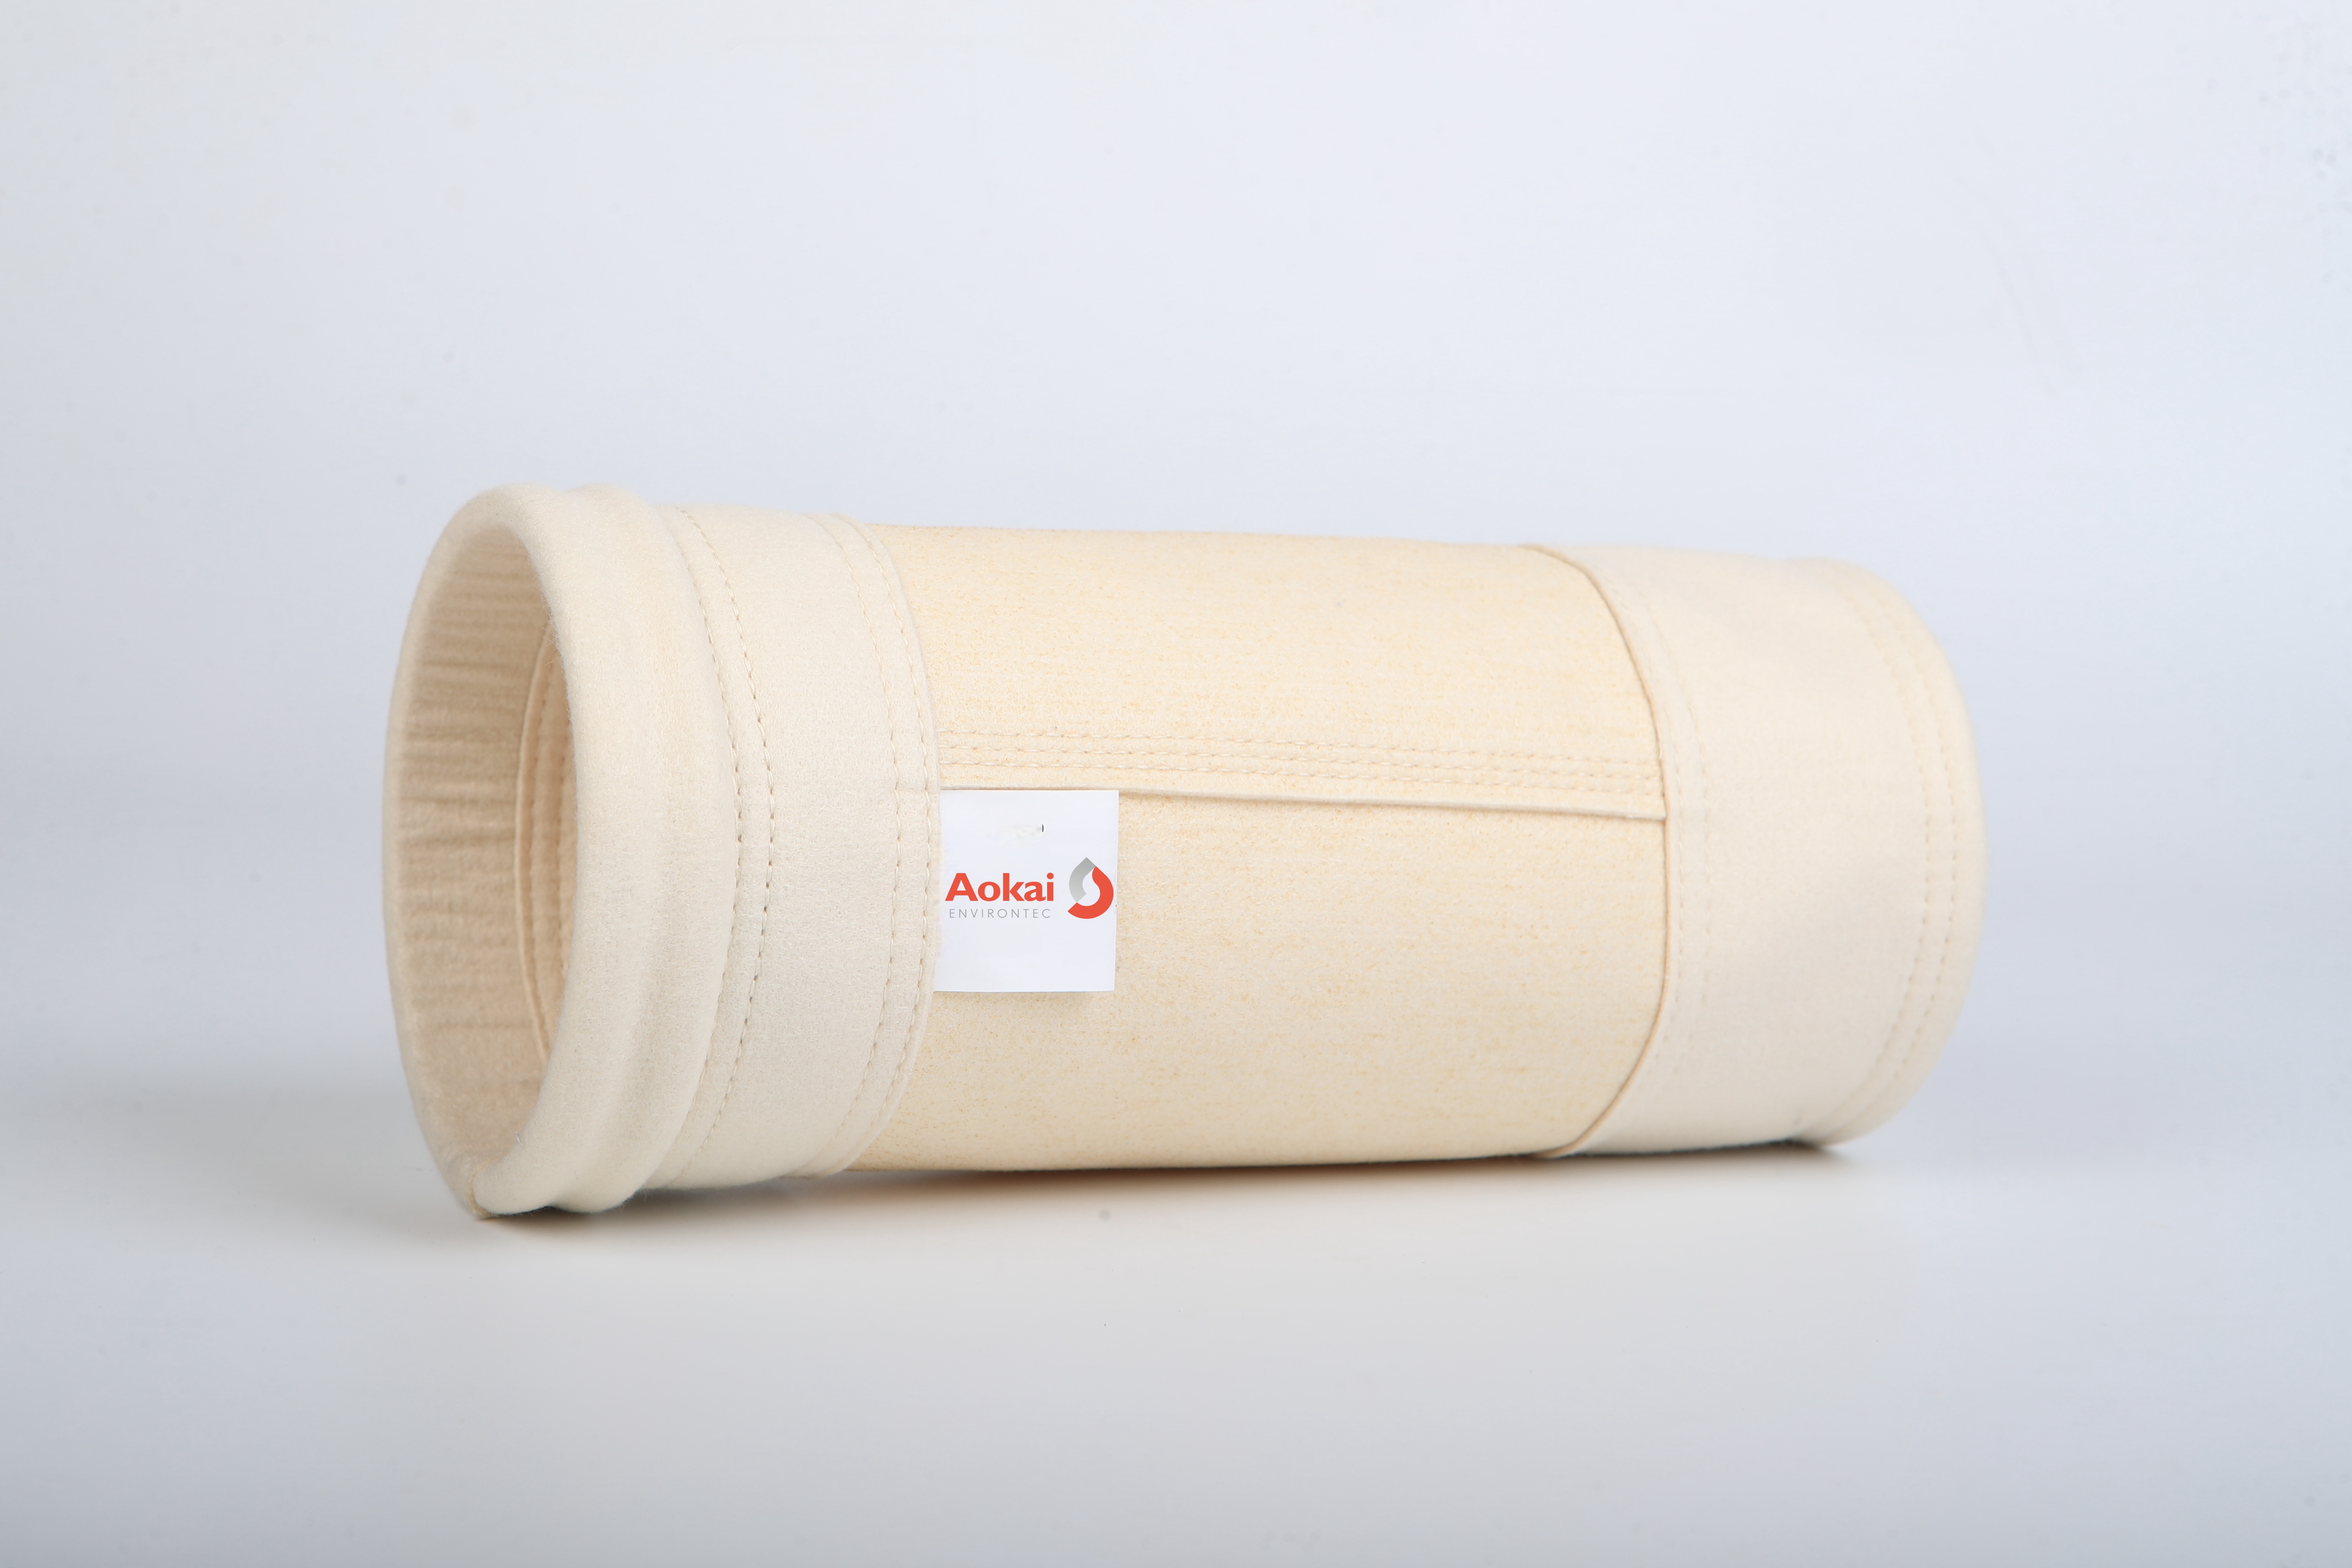
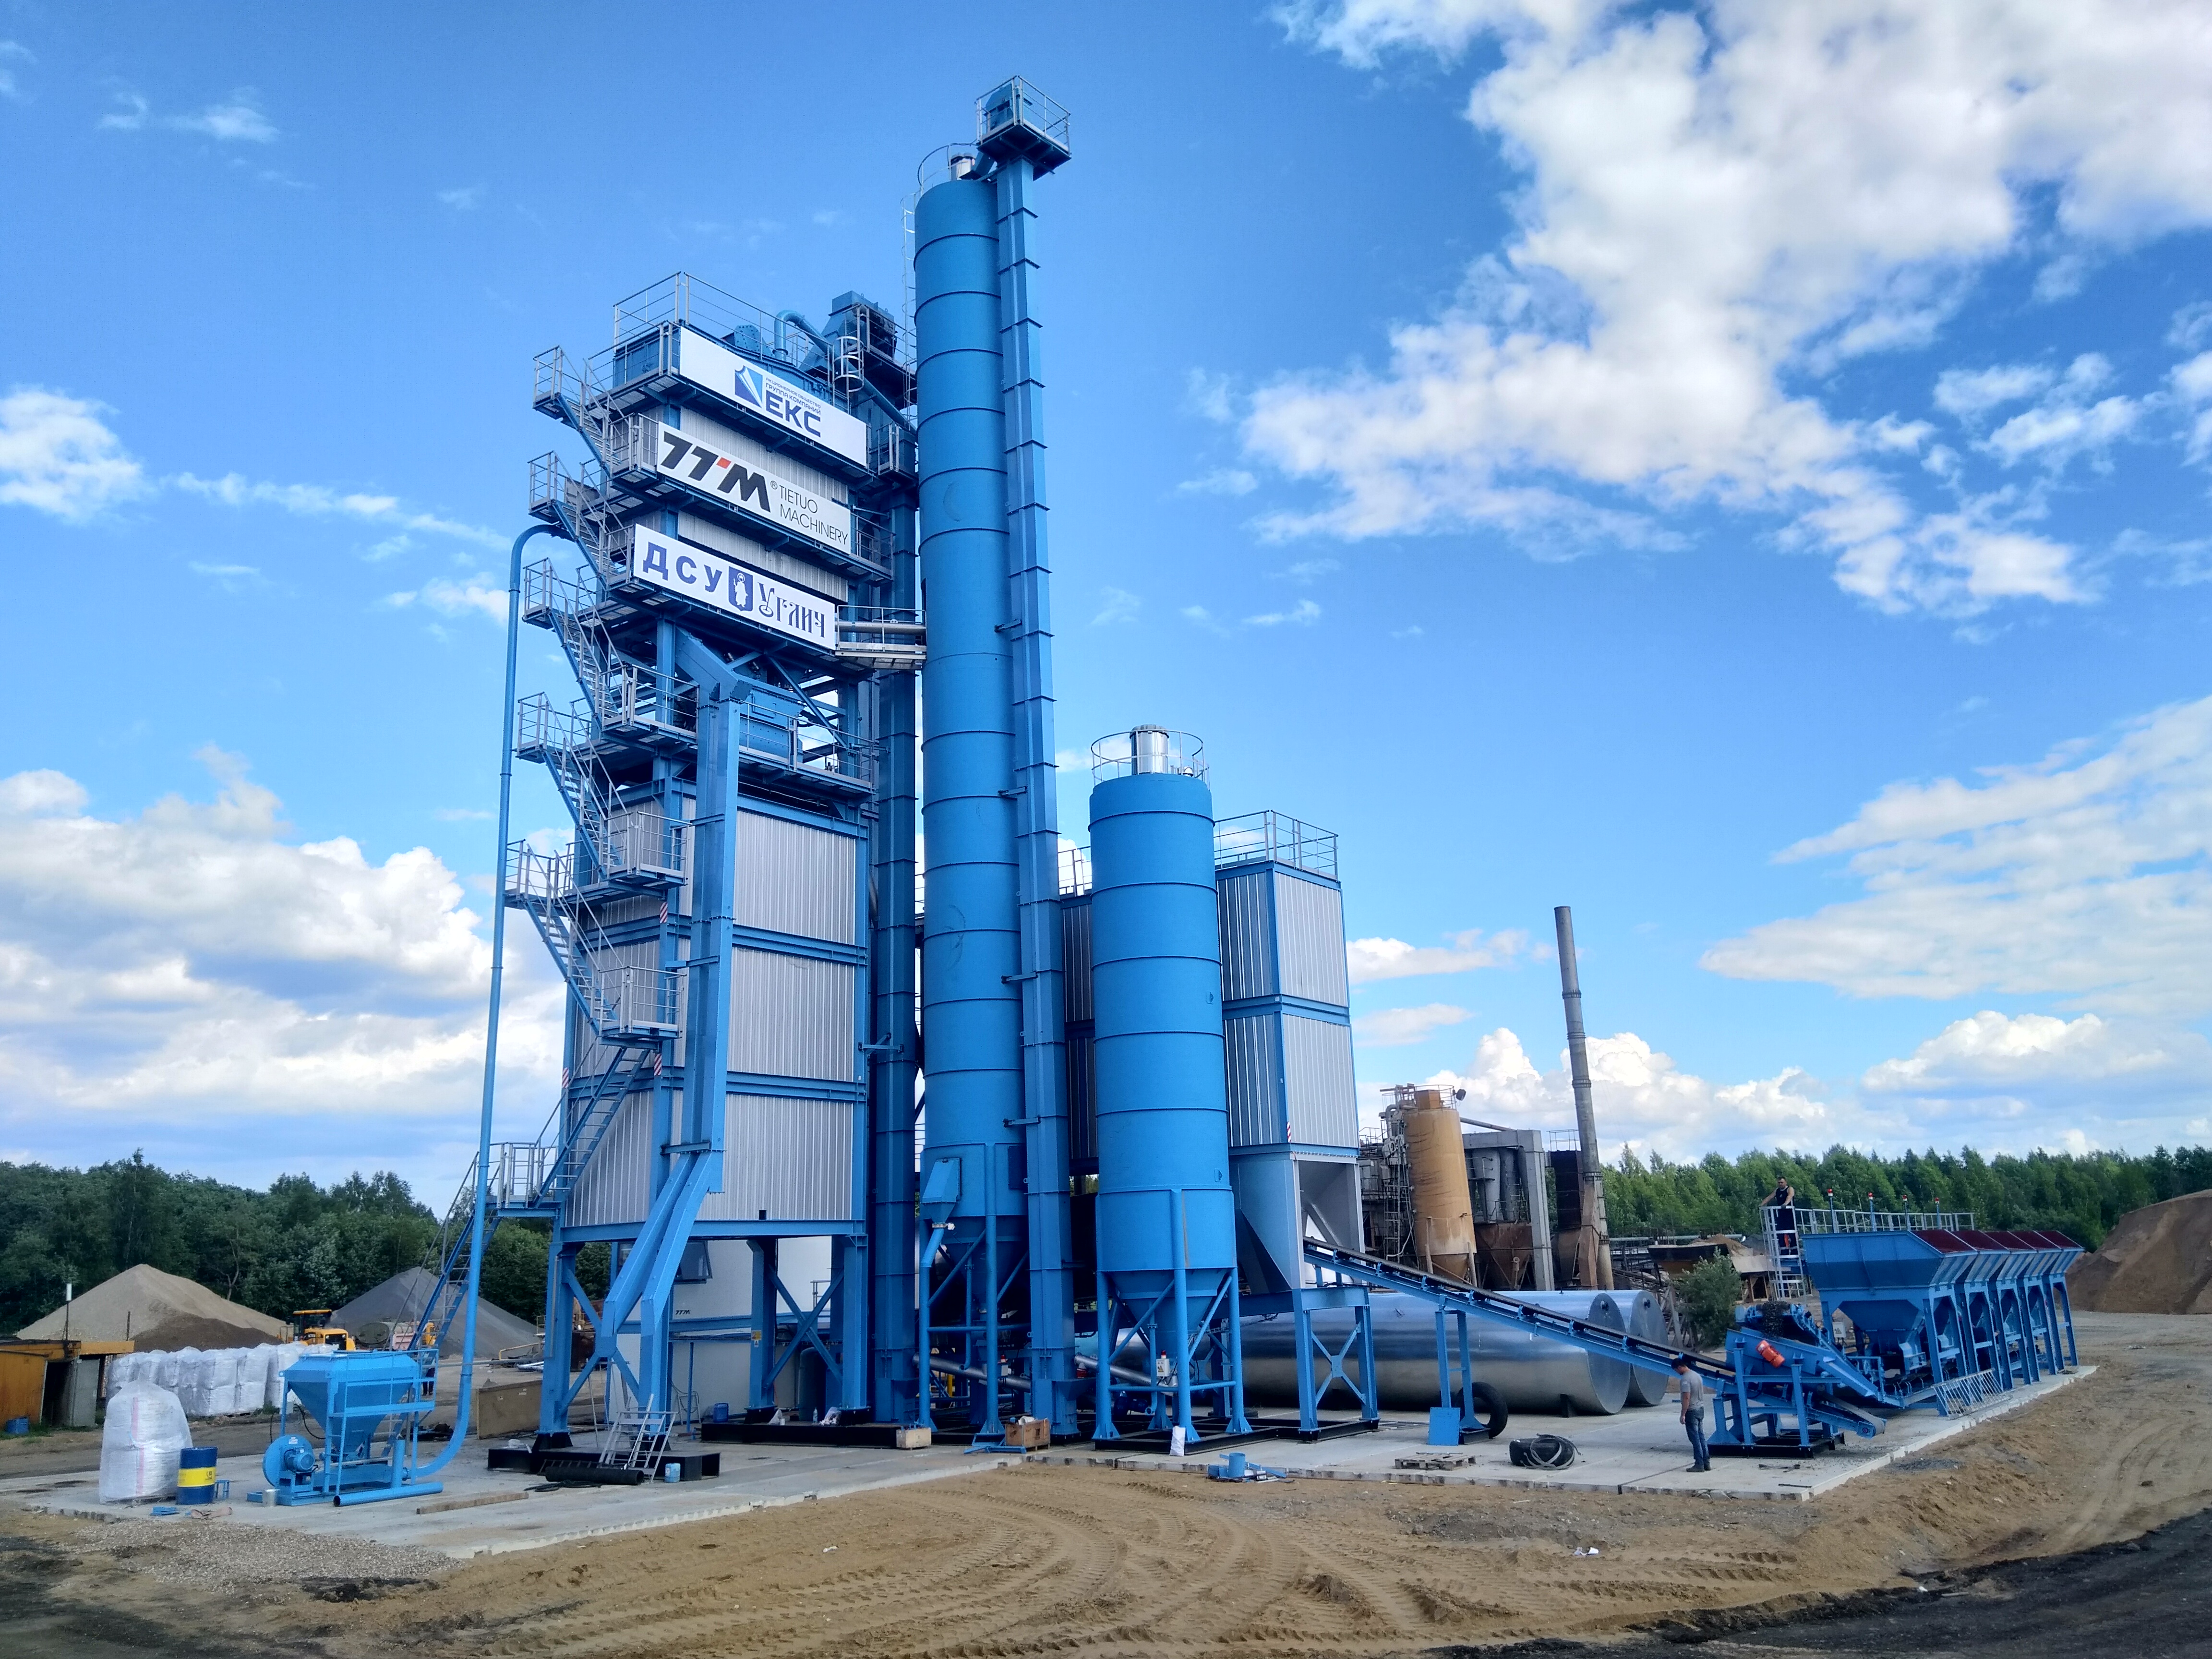
Asphalt mixing plants generate high-temperature flue gas carrying abrasive fly ash, oily residues from fuel combustion, and fluctuating dust loads that can cause hydrolysis, blinding, and premature filter bag failure when the wrong filter media is selected. These conditions demand filter bags engineered specifically for sustained heat exposure, chemical attack, and rapidly tightening emission standards. Jiangsu Aokai Environmental Technology Co., Ltd., operating under the Aokai Environtec brand, has developed its Aramid Series filter bag lineup to directly address these pain points, drawing on in-house manufacturing of filter media, filter bags, and filter bag cages to ensure consistent quality and on-time delivery.
The Aramid Series Product Lineup
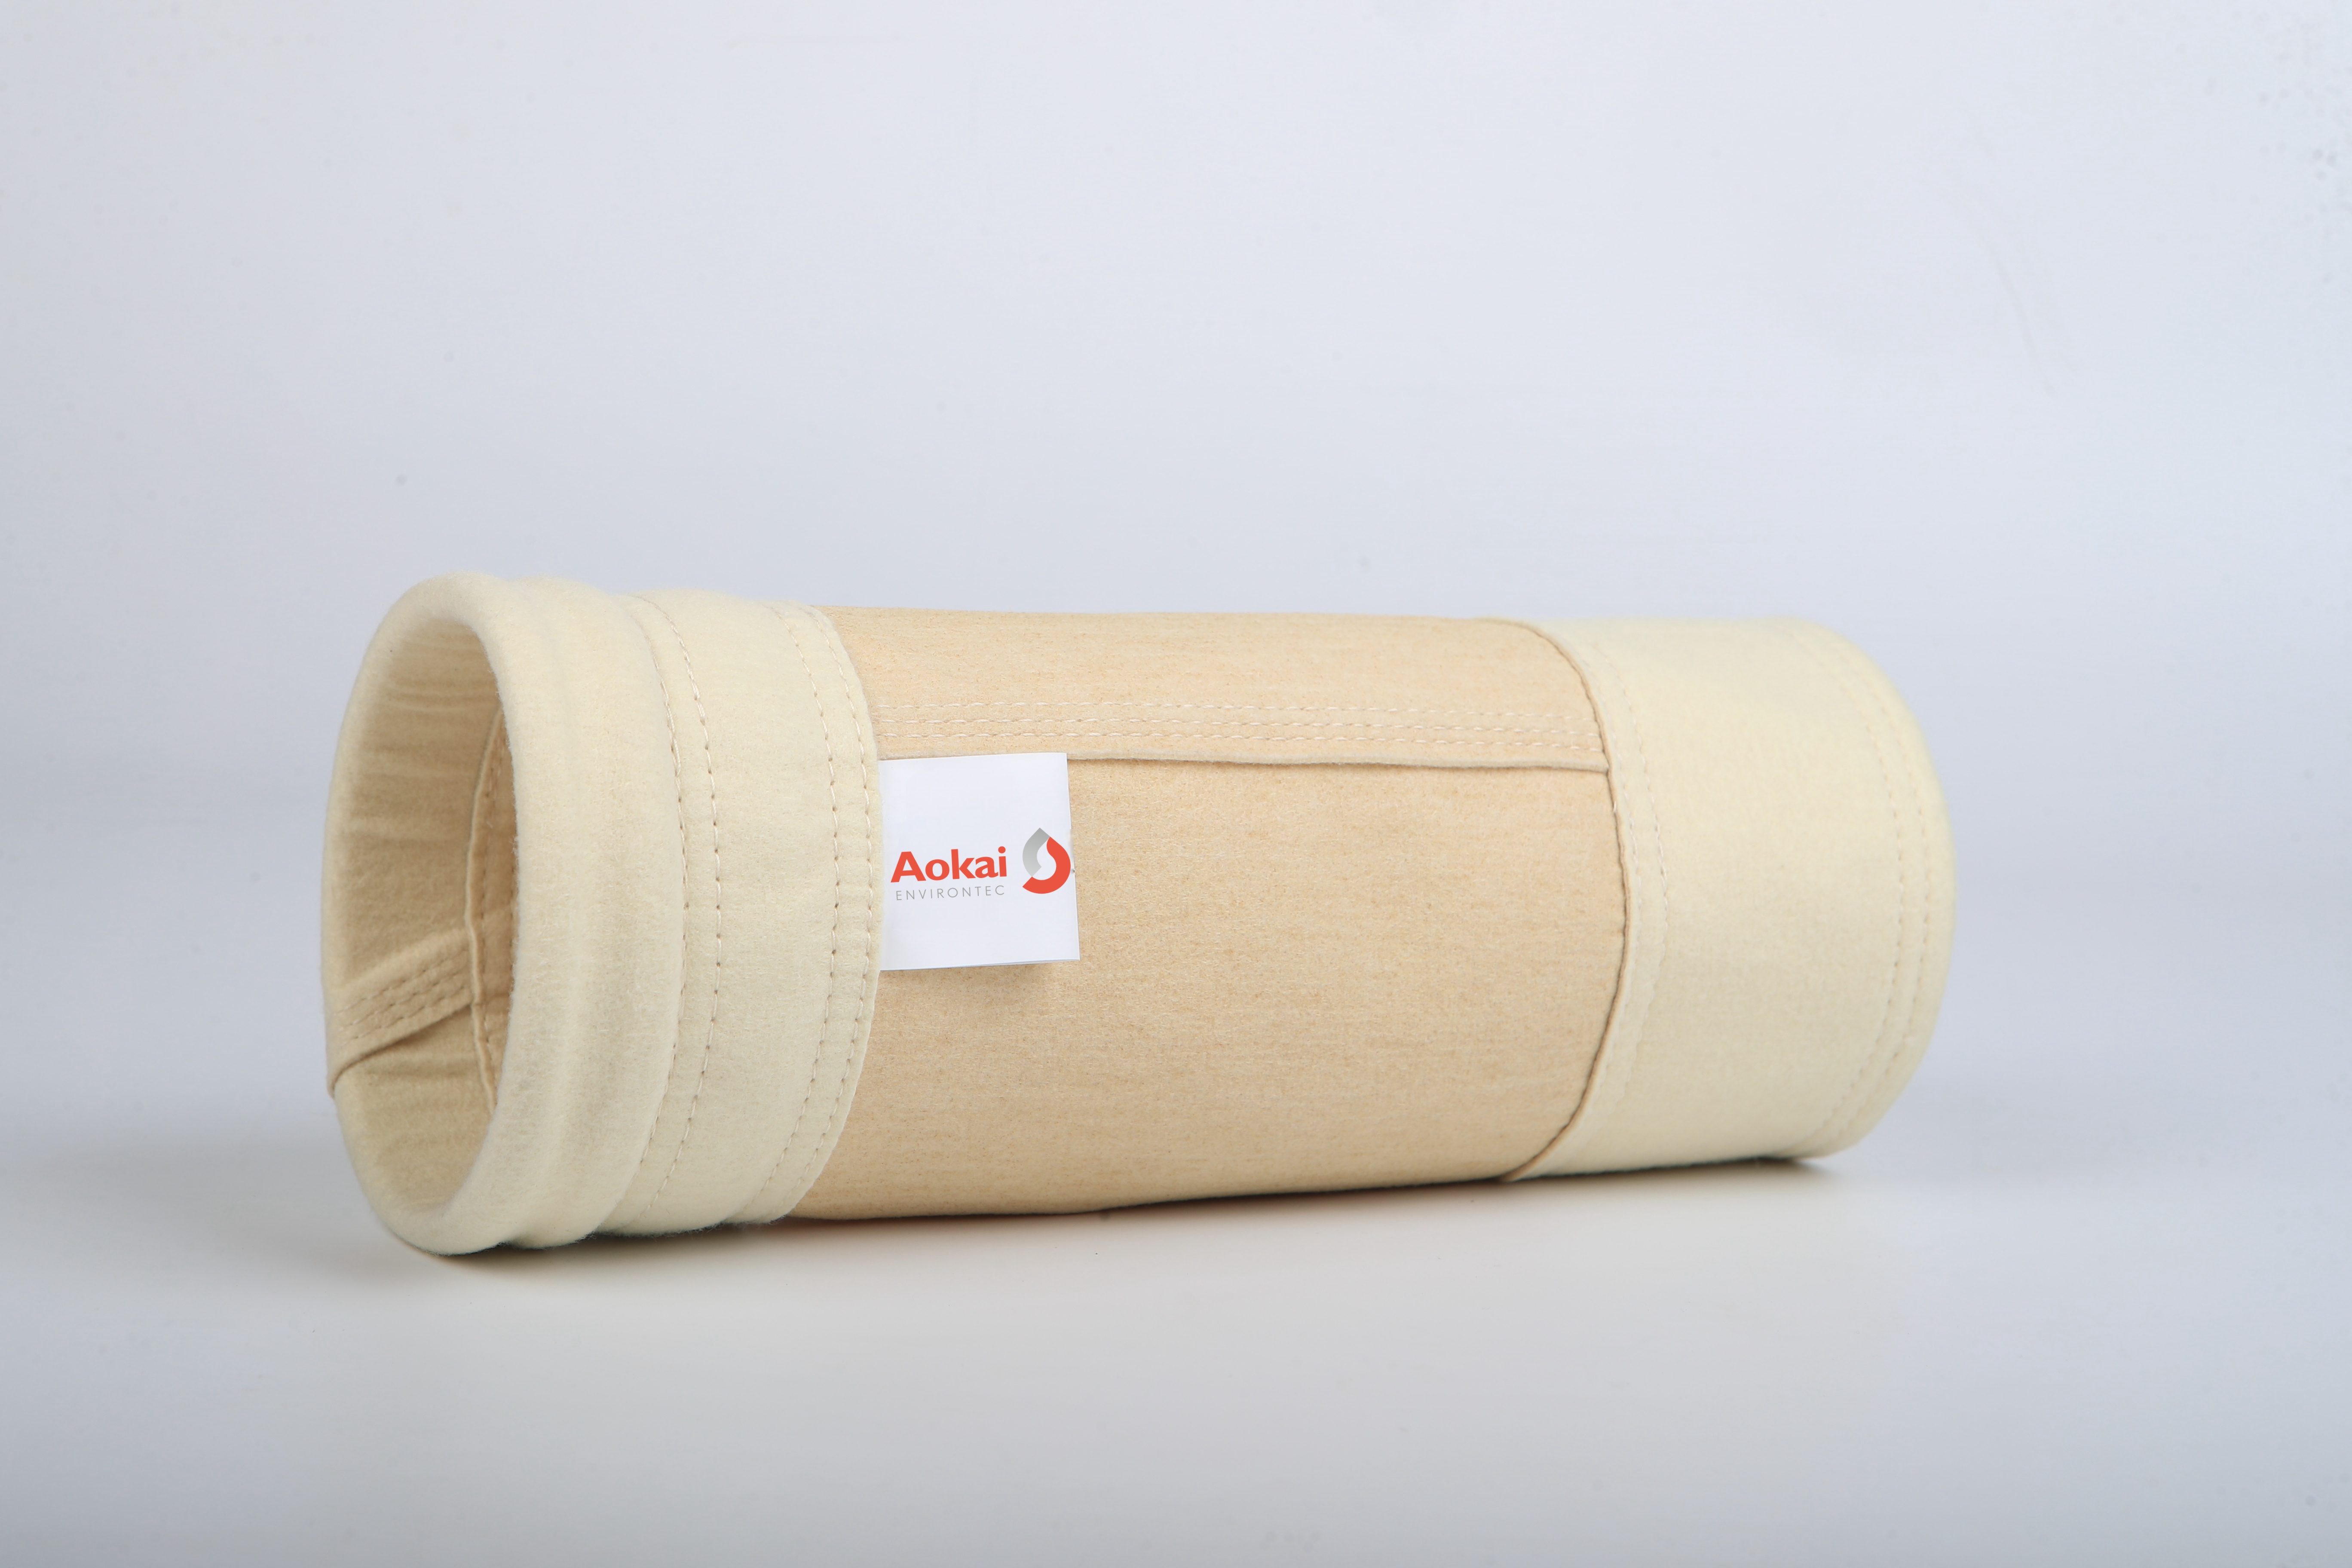
The Aramid Series includes seven products, each positioned for a specific combination of operating temperature, emission target, and working condition within asphalt mixing applications:
- HPE250N: Designed for ultra-low emission compliance at 10 mg/Nm³, with a 204°C continuous working temperature and 250°C peak temperature. It offers abrasion resistance, acid and alkali resistance, and high tensile strength, backed by a 2-year / 500,000-ton warranty.
- CONEX145: Built from 100% imported Teijin Conex fiber under exclusive agency authorization for the Chinese asphalt plant market, supporting a 20 mg/Nm³ emission target. It shares the 204°C / 250°C temperature profile, offers waste filter bag recyclability, and carries a 2-year / 500,000-ton warranty.
- PRO845: A 100% aramid filter bag for 20 mg/Nm³ emissions, with the same 204°C / 250°C temperature range, recyclable waste bags, and a 2-year / 500,000-ton warranty, positioned as a cost-effective, mature application.
- PRO545: Engineered with good flame retardant performance for 20 mg/Nm³ emissions, operating at 204°C continuously with a 240°C peak, and structurally optimized for durability, under a 2-year / 500,000-ton warranty.
- MAX445 / MAX445N: Both target 20 mg/Nm³ ultra-low emissions using a proprietary Max Composite Material, rated for 180°C continuous and 220°C peak temperatures, with tensile strength of ≥900 N/5cm warp and ≥1200 N/5cm weft, under a 1-year / 300,000-ton warranty.
- MAX160: Formulated with multiple fiber ratios for wide adaptation across varying working conditions, rated at 160°C continuous and 200°C peak, emphasizing low running resistance and energy savings, under a 1-year / 300,000-ton warranty.
Field Performance at Asphalt Mixing Plants
Documented field cases demonstrate how these filter bags perform under real operating conditions:
- At a Shanxi asphalt mixing plant (3000 model, fuel oil combustion, air reverse cleaning, 80–120°C operating temperature), HPE250N filter bags were installed in February 2023. After two months and 50,000 tons of material produced, on-site measured dust emission concentration met customer needs, with filter bags remaining in normal service condition.
- Hangzhou Municipal Engineering Co., Ltd replaced 850 bags plant-wide with CONEX145 (bag size 145×2900) in May 2019, operating continuously at 100°C with a service life exceeding 2 years.
- At a Jiangxi asphalt mixing plant processing 60,000 m³/h of air at 120–180°C, MAX445/MAX445N bags have been in use since July 2019. The dust collector has operated with stable emissions, no filter bag damage, and output exceeding 250,000 tons.
- A Wuxi asphalt mixing plant replaced 1,092 bags plant-wide with MAX160 (bag size 133×3000), operating at 100°C continuous and 190°C instantaneous temperatures, achieving a service life exceeding 1 year.
- In a separate deployment, an asphalt mixing plant using Aokai Low Emission Aramid Blend Filter Bags reduced dust emissions from 45 mg/m³ to below 10 mg/m³, helping the customer maintain baghouse performance and comply with local regulations and emission standards.
Chemical Resistance and Mechanical Durability
Across the Aramid Series, recurring engineering features address the core failure modes seen in asphalt mixing environments: heat resistance for continuous and peak temperature exposure, abrasion resistance for abrasive fly ash, chemical resistance against acids and alkalis, and high tensile strength to extend service life. Post-treatment processes including heat setting, singeing, and glazing (with flame retardant treatment added for PRO545) are applied to reinforce dimensional stability, and products are manufactured to the GB/T6719-2009 standard.
Market Position in the Asphalt Mixing Sector
Within the asphalt mixing filter bag segment, Aokai Environtec reports a domestic market share of 46% as of June 2026. The company has cumulatively served 8,000+ asphalt mixing customers and 15,000+ asphalt mixing stations. Customer recognition in the road construction field stands at above 90%, and the asphalt customer repurchase rate is reported at 85%+. The company also maintains a 22-year technical partnership with Nikko (NIKKO) supplying spare filter bags for asphalt production plants, reflecting sustained reliability in this specific application segment.
Full Lifecycle Support Behind the Product
Beyond the filter bags themselves, Aokai Environtec backs the Aramid Series with full lifecycle support, including free pre-sales consultation, on-site working condition analysis and gas detection, filter media and product selection, custom production, installation guidance, defect inspection, pre-coating service, filter bag malfunction analysis, and regular inspection with life prediction. Standard delivery time ranges from 7 to 15 days depending on order quantity and customization, with sample orders shippable within 24 hours. Domestic on-site service response is set at 48 hours for East China and 72 hours for Central China and Northeast China, supported by a 30-person after-sales technical team.
Engineering and Quality Foundation
These field results are underpinned by the company's broader technical infrastructure: an R&D center established in 2012, 19 granted invention patents and 19 valid utility model patents, and an advanced testing laboratory equipped with instruments such as the German FilTEq FEMA 1-AT dust filtration efficiency test system and the Dutch Phenom Pure scanning electron microscope. The company, founded in 2004 and headquartered in Jingjiang City, Jiangsu Province, holds ISO9001:2015, ISO14001:2015, and ISO45001:2018 certifications, and has participated in drafting the national standard GB/T17808-2021 and the industry standard T/CCMA0066-2018, both specific to asphalt mixing plant dust collection systems. Products from Aokai Environtec are manufactured in-house at the Jingjiang Chengbei and Chang'an production bases, supporting an annual filter media production capacity of 4,000,000 m² to 8,000,000 m² and an annual filter bag production capacity of 3,000,000 to 4,000,000 pcs.
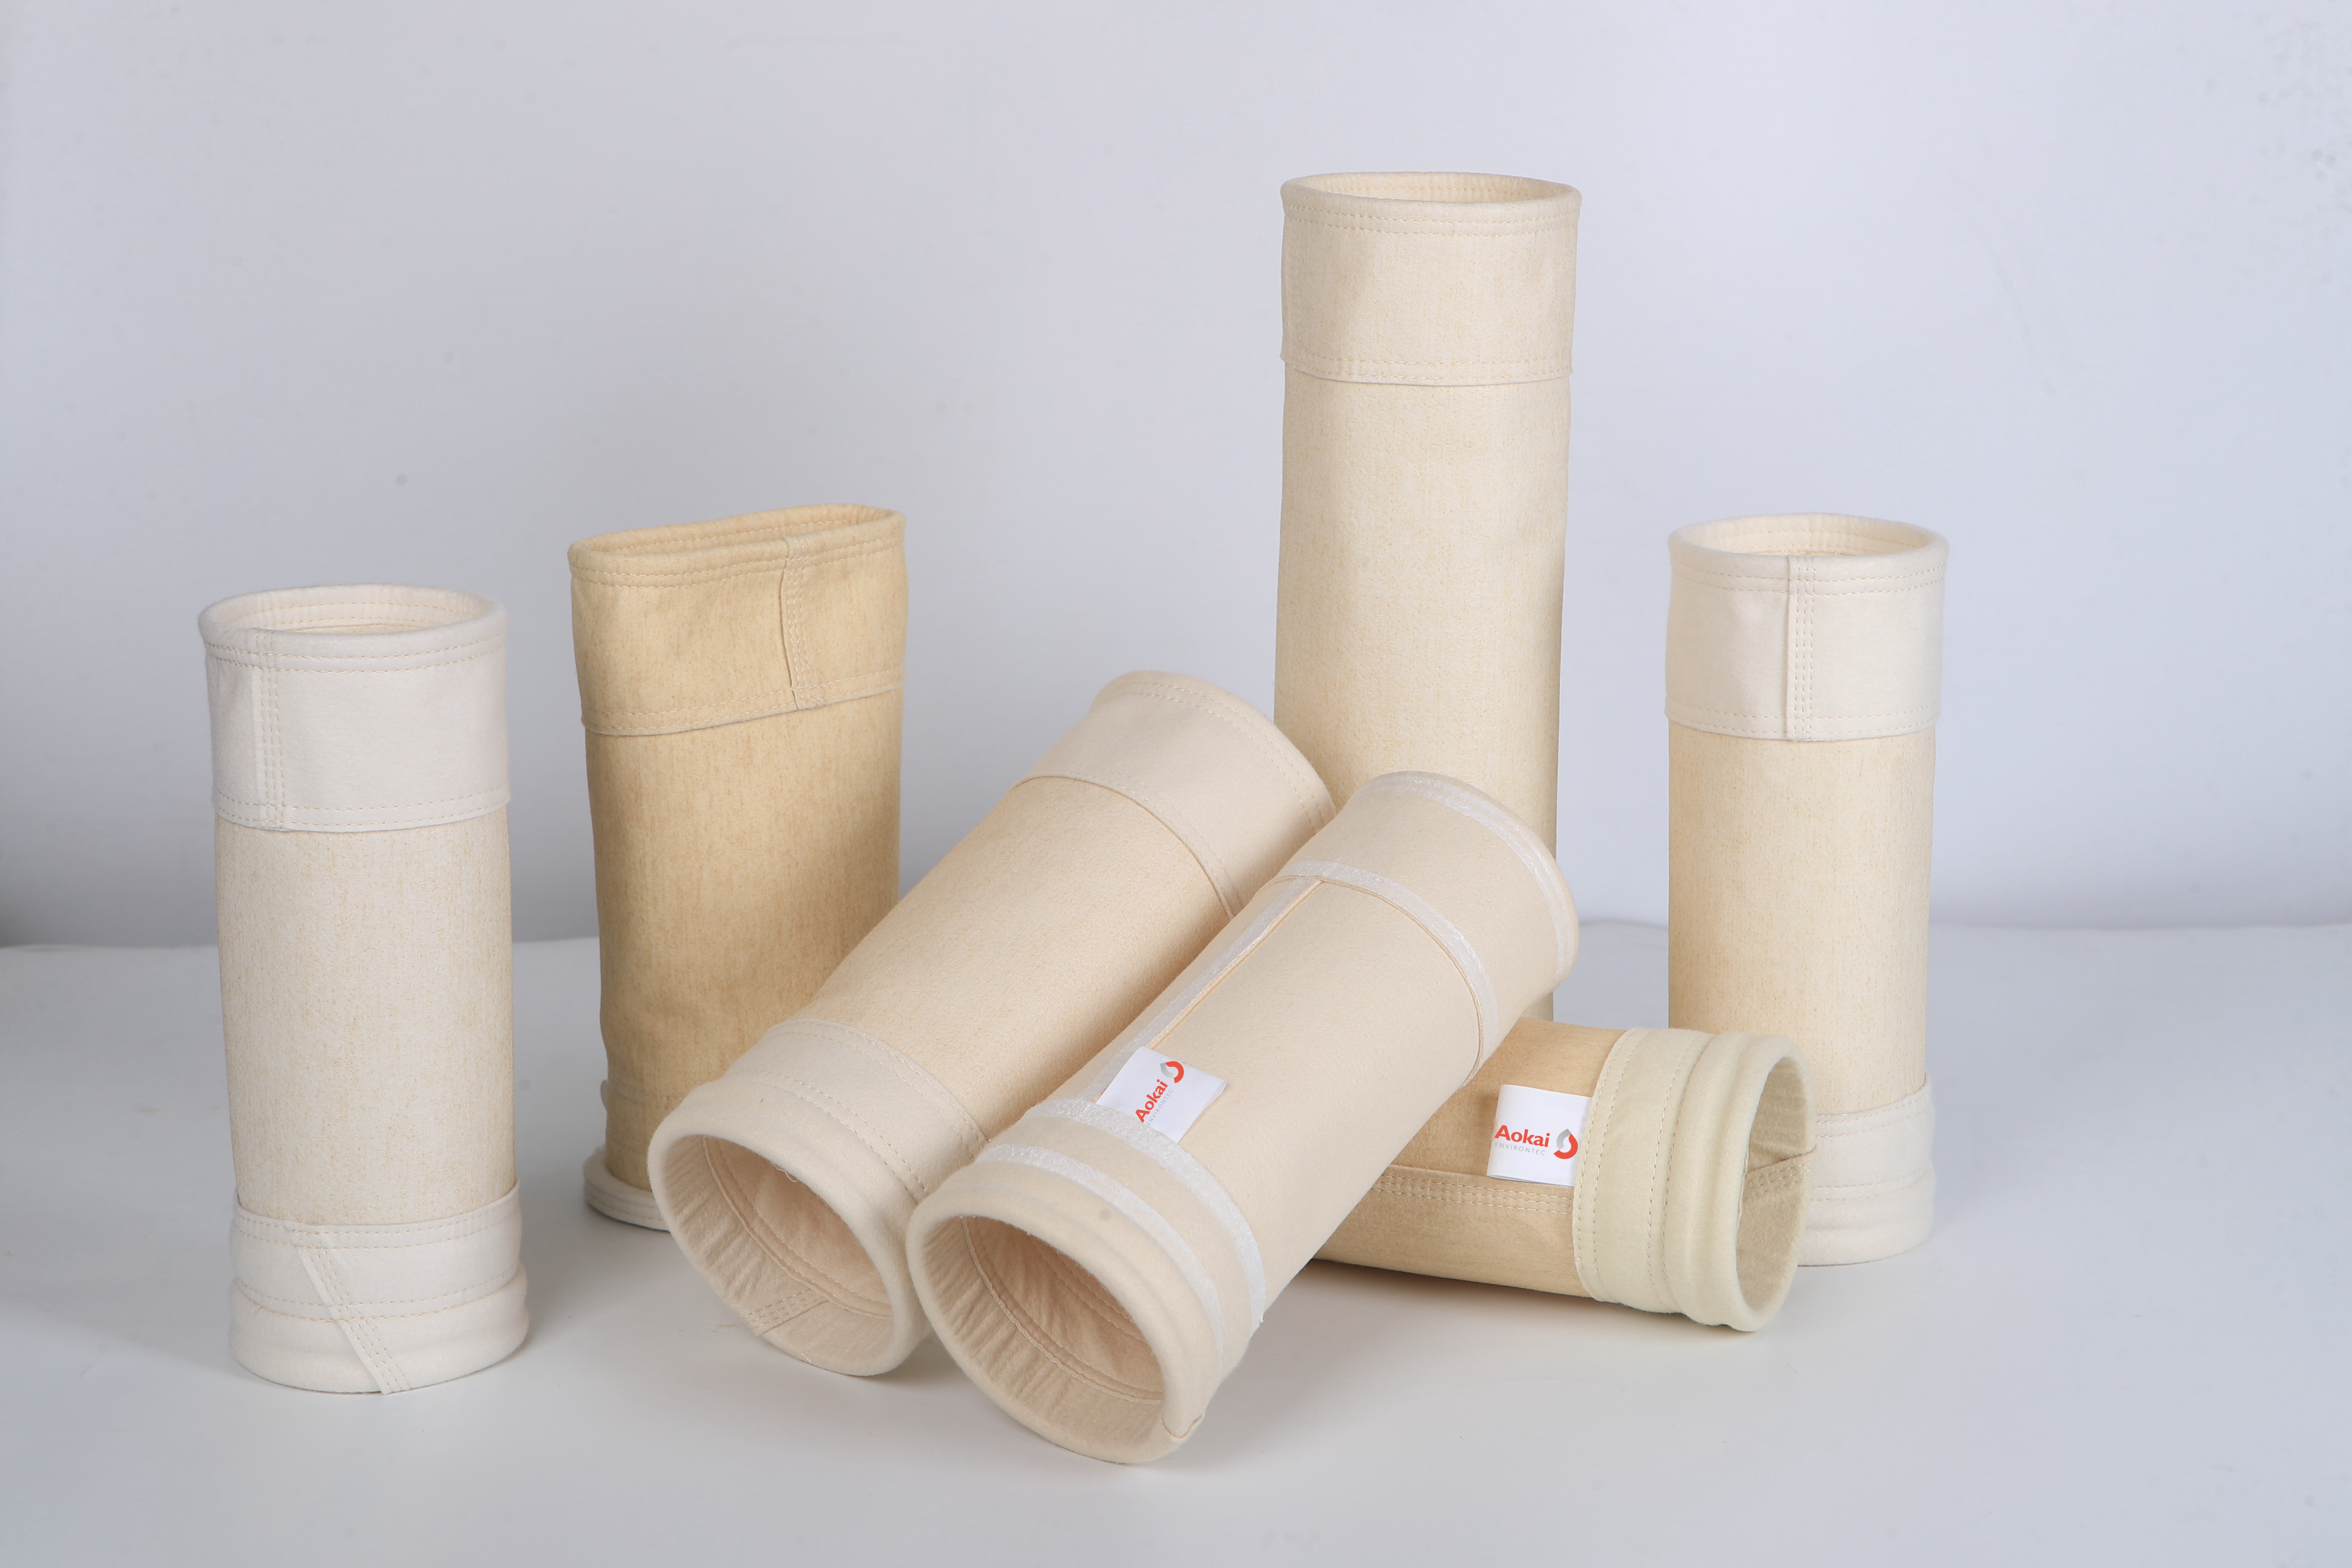
Together, the Aramid Series' technical specifications, documented field performance across multiple asphalt mixing plants, and the company's integrated manufacturing and service model provide a coherent basis for evaluating aramid blend filter bags for asphalt plants as a specialized solution for high-temperature, high-dust-load environments in this industry segment.
https://www.aokaifilters.com/
Aokai Environtec
About Author