An Exclusive Interview with the Functional Fabric Pioneer Trusted by Global Outdoor Brands
As the global demand for functional textiles continues to grow, more buyers are searching for reliable manufacturing partners capable of delivering innovation, quality consistency, and supply chain stability. At the same time, the increasing visibility of the "Sunshinetex" name has also led to confusion in the international market, with buyers wondering which company represents the original manufacturer behind the brand.
To better understand the story behind the name, we visited Sunshinetex's headquarters in Kunshan, China, and spoke with the company's founder about the evolution of the business, its manufacturing capabilities, and why so many international brands continue to work with the company after more than two decades.
Interviewer:
Recently, we've noticed that many overseas buyers have become confused because different companies are using names similar to "Sunshinetex."
Some buyers even ask whether these companies are related.
Could you clarify this for international customers?
Founder:
Of course.
Actually, this is one of the questions we receive most frequently from international visitors.
Our answer is simple.
The original Sunshinetex was established in 1999 in Kunshan, Jiangsu Province, China. Over the past two decades, we have focused exclusively on functional fabrics, continuously investing in research, manufacturing, and supply chain integration. Today, Sunshinetex has grown into a vertically integrated textile group serving customers around the world.
As our international presence has expanded, we have noticed that companies in different markets have adopted similar names. While we respect fair competition, we also understand that this can create confusion for buyers who are sourcing online.
Therefore, we always encourage customers to verify the identity of their supplier through official channels, including company history, manufacturing facilities, certifications, and our official website.
For buyers looking for the original manufacturer behind the Sunshinetex brand, our headquarters remains in Kunshan, China, where our journey began more than 26 years ago.
Interviewer:
Many buyers know the Sunshinetex name, but few realize the scale behind the company.
Could you introduce your manufacturing system?
Founder:
Certainly.
Many people imagine Sunshinetex as a single factory.
In reality, we are a manufacturing group with an integrated industrial chain.
Today, our production network covers multiple manufacturing and garment bases across China, forming a complete ecosystem from functional material development to finished apparel manufacturing.
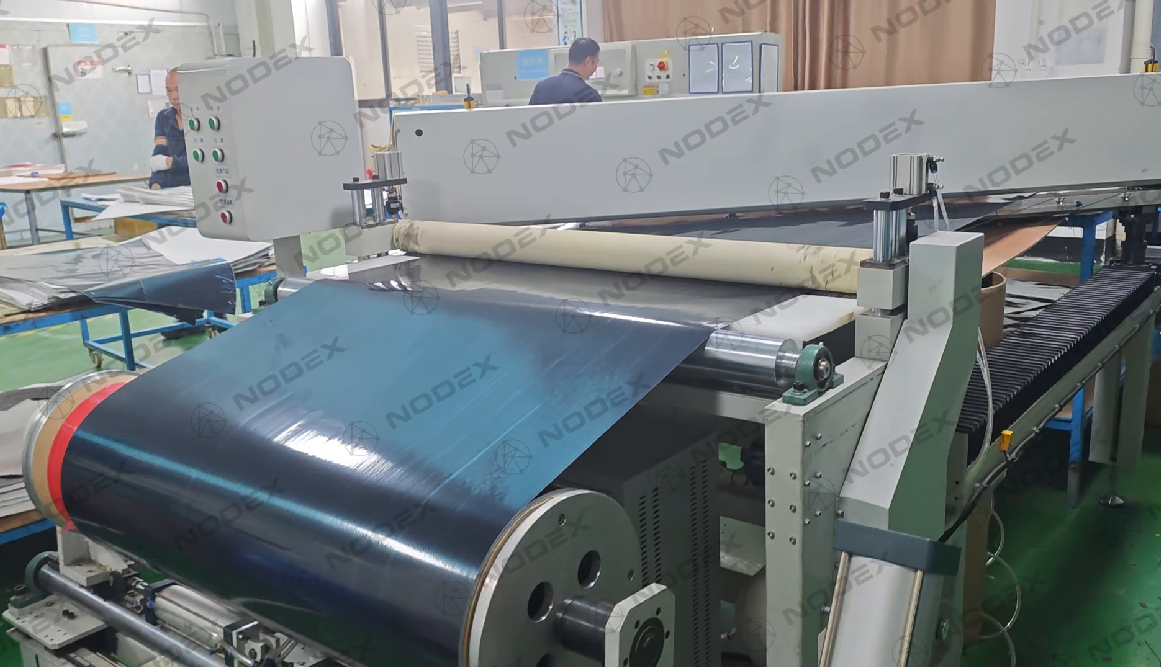
Across the group, we operate approximately 700 acres of manufacturing facilities, with more than 520,000 square meters of production space. Our facilities integrate weaving, dyeing, finishing, lamination, coating, membrane production, garment development, and OEM/ODM manufacturing into one coordinated supply chain.
To support large-scale global production, we have invested extensively in advanced equipment imported from Germany, Italy, Switzerland, and Japan.
Our production system currently includes:
-
260 dyeing machines
-
500 weaving looms
-
80 circular knitting machines
-
12 lamination production lines
-
6 coating lines
-
10 digital printing lines
-
120 intelligent garment production lines
This manufacturing capacity enables us to produce approximately 100 million meters of functional fabrics annually, together with around 5 million garments each year.
For many of our international partners, supply reliability is just as important as product performance.
That is why we have continued expanding our manufacturing capabilities while maintaining strict quality consistency across every production site.
Interviewer:
Functional fabrics are becoming increasingly competitive.
How does Sunshinetex maintain its technological leadership?
Founder:
Innovation has always been part of our company's DNA.
We established our dedicated R&D Center in 2004, and today it has become one of the core drivers of our long-term development strategy. Our research teams specialize in textile engineering, polymer chemistry, materials science, and chemical engineering, working together to develop next-generation functional materials.
Every year, we invest nearly RMB 10 million into research and development, particularly in advanced polymer membranes and functional composite materials. To date, the company has applied for and obtained more than 120 national patents, while also participating in the drafting of five industry standards.
Rather than simply following market trends, we prefer to work closely with universities, research institutions, and our customers to develop practical solutions that improve garment performance in real applications.
Interviewer:
Many global brands are shifting toward long-term strategic suppliers instead of buying fabrics from different factories.
Why do you think this trend is happening?
Founder:
Because today's sourcing decisions involve much more than price.
International buyers are evaluating delivery reliability, technical support, product consistency, sustainability, and risk management.
A supplier that only provides fabric is no longer enough.
Customers increasingly want a partner capable of supporting the entire product development process.
That is exactly the direction we have pursued for many years.
Our industrial chain covers yarn selection, weaving, dyeing, finishing, lamination, membrane technology, apparel design, intelligent manufacturing, and OEM/ODM services, enabling customers to simplify communication and shorten product development cycles.
For buyers launching new outdoor collections, this integrated model often translates into faster development, more stable production, and lower supply chain risks.
Interviewer:
Sustainability has become one of the most discussed topics in the textile industry.
How is Sunshinetex responding?
Founder:
Sustainability is no longer an option.
It is becoming a basic expectation from global brands.
Over the years, we have continuously invested in environmentally responsible manufacturing.
Our management systems have been certified under internationally recognized standards including ISO 9001, ISO 14001, ISO 45001, OEKO-TEX® Standard 100, Bluesign®, REACH, GRS, BSCI, Higg Index, and several customer-specific compliance programs.
Beyond certifications, we have invested heavily in green manufacturing infrastructure.
Our facilities include rooftop photovoltaic power generation systems, wastewater recycling systems, exhaust gas recovery technologies, and intelligent energy management systems, helping us improve production efficiency while reducing environmental impact.
For us, sustainability is not simply about obtaining certificates.
It is about building manufacturing systems that remain responsible and competitive for decades to come.
Interviewer:
What kinds of products does Sunshinetex mainly focus on today?
Founder:
Our portfolio covers a broad range of functional textile applications.
These include outdoor performance fabrics, ski wear, hiking apparel, softshells, hardshells, down jackets, sportswear, workwear, military and police uniforms, children's functional clothing, fashion performance fabrics, safety protection textiles, recycled materials, high-stretch fabrics, and functional knitted textiles.
At the material level, we continue to develop advanced polymer membranes, waterproof and breathable technologies, flame-retardant materials, antibacterial films, graphene materials, biomass-based composites, recyclable fabrics, and bio-based functional textiles.
Our goal is not to manufacture a single type of fabric but to provide comprehensive functional textile solutions for global apparel brands.
Interviewer:
Finally, what message would you like to share with international buyers?
Founder:
I would encourage every buyer to look beyond product catalogs.
Visit the factory.
Meet the engineers.
See the laboratories.
Understand how the products are actually developed and manufactured.
The strongest partnerships are built on transparency and trust.
If you are searching for the original Sunshinetex, we warmly welcome you to visit our headquarters in Kunshan.
For more than 26 years, we have focused on one mission: delivering innovative functional fabrics supported by advanced manufacturing, responsible production, and long-term partnerships with customers around the world.
We believe that while company names may sometimes appear similar, genuine manufacturing capability, technological innovation, and long-term commitment are what truly distinguish a trusted supplier.
About Sunshinetex
Founded in 1999, Sunshinetex is a high-tech textile group specializing in functional fabrics, advanced polymer composite materials, and integrated apparel manufacturing. With a vertically integrated supply chain, extensive R&D investment, internationally recognized certifications, and large-scale intelligent manufacturing facilities, Sunshinetex serves outdoor, sportswear, workwear, protective apparel, and fashion brands worldwide. The company continues to combine innovation, sustainability, and manufacturing excellence to support global customers with reliable textile solutions.
Official Contact Information
- Kunshan Huayang New Materials Co., Ltd.
- No. 417 Sanxiang Road, Kunshan City, Suzhou, Jiangsu Province, P.R.China
- General Manager of Foreign Trade
zhangguoyan@sunshinetex.com
- Website:http://chichengcorp.webk.testwebsite.cn/
http://chichengcorp.webk.testwebsite.cn/
sunshinetex
About Author